If you’re in the business of producing PMMA (acrylic) or PC (polycarbonate) pipes, you already know that even a tiny, easily overlooked part of your pipe making machine can derail an entire production run. I’ve spent over a decade as a supplier of these exact machines, and one question I get asked more than any other is about the lubrication system. “Why does it matter?” “Is it just oil everywhere?” Let me break this down in plain terms—no overly technical jargon, just what actually keeps your PMMA and PC pipes coming out smooth, consistent, and free of defects. PMMA PC Pipe Making Machine

First, let’s ground this: PMMA and PC are unique thermoplastics. They heat to a molten state around 200–280°C, then get extruded, shaped, cooled, and cut into the pipes you sell. The machine that does this has a ton of moving parts working at those high temps: the screw and barrel that melt the plastic, the die that shapes it, the calibrators that hold it to the right diameter, the haul-off unit that pulls it through, and the cutters that snip it to length. None of these parts would last a week, let alone produce high-quality pipes, without a lubrication system tailored specifically to this process—not just a generic industrial lube setup.
Let’s start with the main types of lubrication systems we fit on all our PMMA/PC pipe extrusion machines, and why each is non-negotiable. Most suppliers throw on a one-size-fits-all grease gun setup, but we design ours to be modular, because no two production lines run the same.
The first and most critical is the circulating oil lubrication system for the barrel and screw assembly. Wait, why not just grease that part? Because the screw and barrel are operating at 200°C+—grease would turn to sludge, cook, and gum up the works within hours, not weeks. Circulating oil is a continuous loop: we pump high-temperature synthetic oil (think PAO-based or ester-based, made for heavy-duty extrusion) through jacketed lines that wrap around the screw and barrel, and also through channels drilled into the screw itself. Wait, no—wait, actually, the barrel has internal cooling channels too, right? The oil circulates through the gaps between the barrel wall and the heating zones, carrying away excess heat that would cause the plastic to degrade (PMMA can yellow if it overheats, PC gets brittle) and also reducing friction between the rotating screw and the stationary barrel. If you don’t lubricate this part, friction builds up, the screw bends, and suddenly you’re scrapping entire production batches because the pipe wall thickness is off by millimeters. I’ve seen this happen to a customer in Ohio a few years back—they bought a cheap machine with a cheap lube system, and the screw seized mid-run, turning a 12-hour production of 6-inch PMMA pipes into a pile of useless molten plastic. That’s the cost of cutting corners on the lube system.
Next, we have the grease lubrication system for the low-temperature moving parts. These are the parts that don’t sit at 200°C: the haul-off tracks, the calibration table rollers, the cutter blades’ pivot points, and the gearboxes that drive the entire line. For these, we use high-temperature lithium complex or polyurea grease—made to handle ambient temps in a factory, plus the minor heat they pick up from being near the extrusion line. The key here is that this system is automated, not manual. We fit a central grease pump that’s programmed to dispense exact amounts of grease to each bearing every 45 minutes, depending on production speed. No more operators forgetting to grease a roller for three shifts, leading to premature wear and a wobbly haul-off that makes pipes egg-shaped. I always tell my customers: manual grease jobs are the #1 cause of unscheduled downtime for their pipe lines. Our automated system eliminates that, and we even include a sensor that alerts operators if a grease line is clogged—no more guessing if the lube is actually getting to the parts that need it.
Wait, there’s a third part that a lot of new machine builders skip, and it’s a game-changer for PMMA and PC pipe quality: the air-oil mist lubrication system for the die and calibrator components. The die is what shapes the molten plastic into the pipe’s outer and inner diameters, and the calibrator pulls it into a consistent shape right after extrusion. These parts are at high temps, but they’re also in contact with the molten plastic, so regular oil or grease can get transferred to the pipe’s surface, causing cosmetic defects like streaks or unevenness. Air-oil mist is perfect here: we mix a tiny amount of food-grade (if you’re making pipes for food packaging, or even regular industrial grade) synthetic oil with compressed air, and spray a fine mist directly onto the die and calibrator surfaces. The mist evaporates almost instantly, leaving a microscopic layer of lubrication to prevent the molten plastic from sticking, but no residue left on the pipe. That’s why our customers tell us their PMMA pipes have 30% fewer surface defects than when they used old machines. I can’t tell you how many times a customer has come to us with streaky, scrappy pipe, and after switching to our air-oil mist system, their yield jumped from 82% to 97% in the first month.
Now, let’s talk about why lube system maintenance isn’t just “add oil when it’s low.” A big mistake I see new owners make is using the wrong oil. For example, if you use a mineral-based oil in the circulating system for a PC pipe line, at 250°C that oil will break down into carbon deposits in just a few days. Those deposits get into the screw, and they can abrade the plastic as it’s being extruded, leading to tiny black specks in the pipe—totally unacceptable for premium industrial or consumer pipes. That’s why we specify exactly what lube to use, and we include built-in filtration systems in the circulating loop. The filter traps metal shavings from wear in the screw and barrel, and even tiny plastic particles, so they don’t circulate back and cause damage. We also program the machine’s HMI (human-machine interface, the touchscreen you use to run the line) to alert you when oil levels are low, when filters need changing, or when the grease pump is due for a service. No more guessing—our machines track all that for you, which cuts maintenance time by 40% compared to older models.
Let me also clear up a common myth: some people think that because PMMA and PC are plastics, you don’t need to lubricate the process, just the machine. That’s half wrong. The interaction between the moving metal parts and the molten plastic creates a ton of friction—even if the plastic itself is slippery. If there’s no lube on the screw, the screw can’t rotate evenly, so the plastic is extruded at inconsistent rates, leading to pipes with varying wall thickness. That’s a huge issue for customers who use these pipes for things like automotive components or medical tubing, where wall thickness has to be within 0.1mm tolerance. Our lube system keeps the screw rotating smoothly, so extrusion is consistent, and that consistency translates directly to better pipe quality.
Now, I know you’re probably wondering: how does this all work in real time on a production run? Let’s walk through a typical 8-hour run of 4-inch PMMA pipes, for example. The machine heats the barrel to 240°C, the circulating oil system kicks on, pumping synthetic oil through the barrel’s jacket. As the screw turns pushing molten PMMA toward the die, the oil carries away excess heat, keeping the barrel at a steady temp. The air-oil mist system is spraying a fine mist on the die, so when the molten PMMA comes out, it doesn’t stick, and forms a smooth, uniform pipe wall. The calibration table rollers are getting greased automatically every 45 minutes, so they roll smoothly, keeping the pipe straight as it’s pulled by the haul-off unit. The cutter’s pivot points are greased too, so the blades make clean, even cuts, no jagged edges on the pipe ends. Everything works in sync, no hiccups, no downtime, no scrapped pipes.
As a supplier, I don’t just sell machines— I sell the peace of mind that your production will run smoothly. I’ve seen so many customers get burned by cheap machines with cheap lube systems that break down after a few months, leading to thousands in lost revenue and repair costs. That’s why we spend so much time designing the lube system to be robust, tailored specifically for PMMA and PC pipes, and easy to maintain. We don’t cut corners on parts—we use brand-name pumps, filters, and oils that are built to handle the harsh extrusion environment.
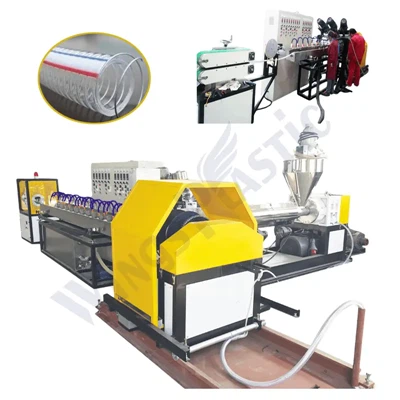
If you’re in the market for a PMMA or PC pipe making machine, don’t sleep on the lubrication system. It’s not a “side feature”—it’s the backbone of your line’s efficiency, quality, and longevity. If you have questions about how our lube system works, or want to hear more about how it’s helped other customers boost their yield, feel free to reach out. We can walk you through specs, show you case studies, and answer any questions you have about making the best PMMA and PC pipes possible.
PVC Hose Machine References
- Giles, H. F., Wagner, J. R., & Block, H. (2014). Extrusion: The Definitive Processing Guide and Handbook (2nd ed.). William Andrew.
- Rosato, D. V., & Rosato, M. G. (2004). Thermoplastics Processing Handbook. Springer.
- Society of Plastics Engineers. (2021). Extrusion Lubrication Best Practices for Thermoplastic Processing. SPE Journal.
- Brannon, R. B. (2019). High-Temperature Lubrication for Industrial Extrusion Equipment. Tribology Transactions.
- American Society for Testing and Materials. (2020). Standard Specification for Polycarbonate (PC) and Acrylic (PMMA) Plastic Pipe and Tubing. ASTM D1785 / D2241.
Qingdao Wings Plastic Technology Co., Ltd.
As one of the most experienced pmma pc pipe making machine manufacturers and suppliers in China, we also support customized service. Please feel free to buy durable pmma pc pipe making machine made in China here from our factory. For price consultation, contact us.
Address: C02 Of Anshengyi Road, No.2 Fuan Industry Zone,Jiaodong Town, Jiaozhou City, Qingdao City, Shandong Province,China
E-mail: kelly@wingsplastic.com
WebSite: https://www.wingsextruder.com/
