Alright, let’s cut to the chase here—if you’re a driving chain supplier, you’ve probably gotten at least a dozen emails this month alone from people asking, “Can my driving chain handle a corrosive environment?” And honestly? It’s one of those questions that sounds super simple on the surface, but it’s way more nuanced than you think. I’ve been in this game for 12 years now—first as a floor hand in the factory, then moving into sales, and now I’m the guy you talk to when you need a chain that doesn’t rust out mid-job. I’ve seen everything from food processing plants that spit out acidic steam to marine rigs that sit in salt spray 24/7, and let me tell you: the answer isn’t a flat yes or no. It’s “it depends on how you set it up, and which chain you pick.” Driving Chain

First off, let’s get one thing straight: corrosive environments don’t play around. I’ve had a customer who runs a chain in a pickle line (think vinegar and brine for veggies) call me in a panic because their $2,000 custom chain turned into a pile of rust slop in 6 months. Another guy runs a chain on a fishing trawler, same basic chain, and it’s still going strong after 4 years. What’s the difference? Two things: the chain itself, and how you maintain it. Let’s break that down without getting too tech-jargon-heavy, promise.
First, let’s talk about the types of corrosion you’re actually dealing with, because not all corrosion is equal. You’ve got your general corrosion— that’s the rust you see on a old bike left out in the rain, right? That’s when metal reacts with oxygen and moisture. Then there’s pitting corrosion, which is way sneakier—it eats tiny holes in the metal, so your chain looks fine on the outside but snaps like a twig when you load it. And then there’s galvanic corrosion, which happens when two different metals touch each other in a wet, salty environment—think steel chain on an aluminum sprocket. That’s the stuff that’ll surprise you the most.
So, back to the main question: can a driving chain be used in this kind of environment? Short answer: yes, but not the cheap off-the-shelf chain you grab from the local hardware store. The standard carbon steel driving chain you use for, say, your warehouse conveyor? It’s not built for this. I learned that early on—my first big client was a small food processing plant, and they tried our standard chain for their tomato paste line (which has mild acidity and a ton of moisture). It lasted 3 months. Oops. Then we swapped them for our corrosion-resistant chains, and now it’s been 2 years with just a quick wipe-down once a month.
Let’s talk about the materials we use for these corrosive-friendly chains, because that’s the real game-changer. First up: stainless steel. But not all stainless is the same. A lot of people hear “stainless” and think it’s indestructible, but no—304 stainless works great for mild corrosion, like if you’re dealing with soda or mild vinegar. But 316 stainless? That’s the heavy hitter. It has molybdenum in it, which makes it perfect for saltwater, strong acids, even some industrial chemicals. I had a customer in the offshore drilling industry who swore by our 316 chains for their pipe handling equipment—they told me once, a piece of debris hit a standard chain on a rig and it snapped, but our 316 one just got a scratch and kept going. The caveat? 316 is pricier, and it’s not invincible to super strong acids or high temperatures, but for most corrosive environments, it’s solid.
Then there’s another option: coated chains. Wait, not just any coating—we’re talking things like zinc plating, but even better, polymer coatings like nylon or Teflon. Wait, but hold up—you can’t just throw a cheap zinc coating on a standard chain and call it corrosion-resistant. We do a full hot-dip galvanize for some of our chains, which means we dip them in molten zinc so the coating seeps into every nook and cranny of the chain links, not just the surface. That’s way better than the thin electroplating you see on cheap chains, which chips off after a few uses and leaves the steel exposed. I’ve seen a customer use our hot-dip galvanized chains for a livestock watering system (which has ammonia from manure—super corrosive) and they’ve been running for 5 years no problem. But coatings have a limit—if you’re running the chain through heavy loads or sharp materials, the coating will wear off, so you have to check it regularly.
Now, here’s the part a lot of suppliers don’t tell you: it’s not just the chain material. It’s the setup and maintenance. I’ve had customers call me saying “your chain is garbage, it rusted in 6 months,” and when I show up to their plant, I see they’re using a standard steel sprocket with their 316 stainless chain. That’s galvanic corrosion right there. The stainless chain is touching the steel sprocket, moisture gets in, and boom—corrosion. Fix that by using a stainless steel sprocket, or a plastic sprocket if the load isn’t too heavy, and that problem goes away. Another big one: lubrication. Regular oil or grease? Not enough in a corrosive environment. We recommend using a food-grade anti-corrosion lubricant for food plants, or a heavy-duty marine grease for saltwater environments. And you can’t just apply it once—you have to do it every couple of weeks, depending on how harsh the environment is. I once had a customer who skipped lubricating his chain because he thought the coating would do all the work—6 months later, the links were seized solid, and he had to replace the whole thing. Don’t be that guy.
Wait, let’s talk about some real-world examples to make this concrete, because numbers and stories stick better. Last year, we got a call from a guy who runs a wood treatment plant—they use a lot of corrosive chemicals to preserve lumber, and his old chain was failing every 4 months. We suggested two options: either our 316 stainless chain, or our hot-dip galvanized chain with a Teflon coating. He went with the galvanized Teflon one, because it was 30% cheaper, and 8 months later, he called to rave about it—no rust, no pitting, he only had to lubricate it twice in that time. Another customer: a brewery, their conveyor carries beer bottles, and the air in the bottling room is moist and has some hops residue (which is slightly acidic). We sold them a 304 stainless chain, and they’ve been using it for 18 months, no issues at all. Then there’s the bad example: a construction company that tried our standard carbon steel chain for a concrete washing station (which has wet cement, super alkaline—really corrosive). The chain rusted so bad the links were stuck together in 2 months. We swapped it for a hot-dip galvanized one, and that’s been good for over a year.
Now, let’s address the myths floating around out there, because I hear them all the time. Myth #1: “Any stainless steel chain works for corrosive environments.” No, like I said, 304 is for mild stuff, 316 is for heavy duty. Don’t waste money on 316 if you only need 304, but don’t buy 304 if you’re dealing with saltwater. Myth #2: “Coated chains never need replacement.” The coating wears down over time, especially if the chain is rubbing against other parts or exposed to abrasives. You have to inspect it every few months. Myth #3: “Driving chains can’t be used in corrosive environments at all.” That’s just not true—we sell hundreds of these chains every year to people in corrosive environments, and 99% of them are happy.
Here’s the thing: as a driving chain supplier, our job isn’t just to sell you a chain. It’s to tell you the truth, even if it means selling you a slightly more expensive chain that lasts longer, instead of the cheap one that will fail in 3 months. Because I’ve seen too many customers lose money from downtime when their chain breaks—like that food processing plant I mentioned earlier, when their chain failed, they had to shut down production for 3 days, costing them $100k. That’s way more than the difference between a cheap chain and a good corrosive-resistant one.
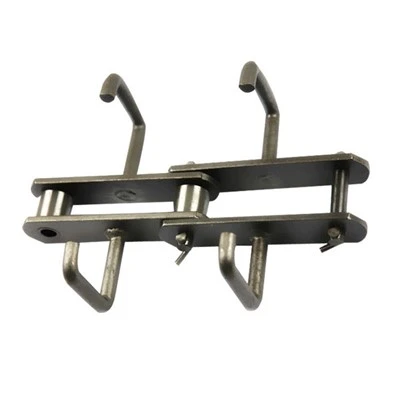
So, if you’re sitting there thinking, “I need a driving chain for a corrosive environment—what do I do?” First, figure out exactly what kind of corrosive environment you’re dealing with. Is it mild (moist air, mild acid) or harsh (saltwater, strong chemicals, alkaline concrete)? Then, reach out to someone who knows driving chains, not someone who just sells generic hardware. We can help you pick the right material, the right coating, the right sprockets, and even give you tips on maintenance. Don’t just guess—ask the experts, because a bad choice will cost you way more in the long run.
Conveyor Chain At the end of the day, can a driving chain be used in a corrosive environment? Absolutely. You just can’t cut corners on the materials, the setup, or the maintenance. I’ve been doing this long enough to know that the guys who succeed in these environments are the ones who invest in the right gear, not the cheap stuff. If you’re tired of replacing chains every few months because of corrosion, hit us up and let’s chat. We’ll hook you up with a chain that actually works for your environment, no fluff, no sales pitch—just real advice from someone who’s seen it all.
References
- NACE International. (2016). Corrosion Basics: An Introduction. Houston, TX: NACE International.
- American Society of Mechanical Engineers (ASME). (2020). Design and Selection of Power Transmission Chains. New York, NY: ASME.
- Stainless Steel World. (2019). “316 Stainless Steel: Performance in Corrosive Environments”. KCI Publishing B.V.
Anhui Huihuang Chain Transmission Co., Ltd.
Anhui Huihuang Chain Transmission Co., Ltd. is one of the most professional driving chain manufacturers and suppliers in China, also supports high quality customized service. Please feel free to buy discount driving chain made in China here from our factory. Welcome to contact us for pricelist and free sample.
Address: NO.3 YONGQIANG ROAD. JIXI.ANHUI.CHINA
E-mail: 754590660@qq.com
WebSite: https://www.hhchains.com/
